Skip to content

In the high-stress environment of a glass tempering furnace, the drive belt system is a critical mechanical link that directly governs rotational synchronization, thermal production efficiency, and the optical surface quality of the finished tempered sheets.
Currently, two distinct belting technologies dominate the ceramic roller conveyors of modern tempering systems: Round Belts and Power Twist Link V-Belts.
This engineering guide provides an objective, comparative analysis of these two components across material properties, mechanical limitations, and operational life cycles to assist plant engineers in optimizing conveyor uptime.
Structural and Material Topology
Circular Section Belts
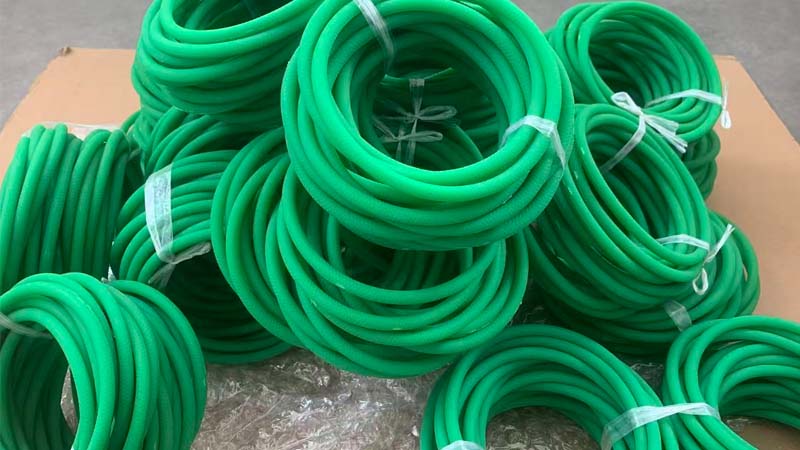
Commonly referred to as polycords or elastomeric O-ring drives, these circular profiles are extruded from thermoplastic polyurethane (TPU). They are either joined on-site via thermal welding or supplied as integrated endless loops.
While certain advanced series incorporate reinforced tensile nylon or steel cores to control elasticity, raw TPU remains highly flexible. This polymer delivers excellent abrasion resistance under ambient factory conditions but faces clear thermodynamic limitations when operating adjacent to furnace heating elements, where continuous radiant heat frequently challenges its standard 80°C thermal threshold.

Segmented Link Belts
The modular alternative represents a transmission drive engineered from individual interlocking component segments. These injection-molded links are mechanically interconnected using integrated twist-lock tabs, completely eliminating the continuous, rigid tension cord found in traditional rubber profiles.
The underlying material architecture consists of a high-performance polyurethane elastomer matrix reinforced with multiple layers of high-tenacity woven polyester fabric. This composite design allows maintenance personnel to manually add or remove individual sections to adjust tension on-demand without specialized joint welding tools.

Mechanical Performance Dynamics
Rotational Synchronization and Surface Tracking
-
Thermoplastic Polycords: Operating via friction within machined round or V-grooves, these circular loops rely entirely on high elastic tension. Because raw TPU naturally softens under continuous radiant heat, solid elastomer lines are highly susceptible to micro-slippage during sudden load changes—such as when a batch of thick, heavy architectural glass transitions onto the roller bed. This momentary lag disrupts roller synchronization, which is a primary mechanical cause of glass surface scratching and tracking misalignment inside the heating chamber.
-
Interlocking Segment Drives: These modular segments lock firmly into standard industrial V-groove pulleys, generating high mechanical wedging force along the pulley sidewalls. The fabric-reinforced composite matrix exhibits virtually zero thermal elongation under standard operational stress. This dimensional stability ensures precise rotational synchronization, maintaining identical surface speeds across all ceramic rollers and mitigating friction-induced surface marking.
Operational Lifespan and Maintenance Cycles
-
Thermoplastic Polycords: Under continuous, round-the-clock industrial duty, standard circular profiles generally provide an operational lifespan of 6 to 12 months. When a thermal weld fails or the material cracks due to heat degradation, the entire loop must be discarded. Furthermore, replacing an endless belt on a multi-roller conveyor often requires partial shaft or bearing disassembly, resulting in extended maintenance downtime.
-
Interlocking Segment Drives: Benefiting from a high-density composite design, premium link belts offer a working life cycle that typically doubles or triples that of standard solid lines. In the event of localized physical damage, technicians can isolate, unlink, and replace only the compromised segments within minutes. To ensure optimal performance post-installation, refer to our mastering Power Twist link belt Instructions.
Engineering Comparison Matrix
| Technical Parameter | Thermoplastic Polycords (Solid) | Interlocking Segment Belts (Modular) |
|---|---|---|
| Material Base | Thermoplastic Polyurethane (TPU) | Polyester-Reinforced PU Composite |
| Elongation Resistance | Moderate; Prone to thermal relaxation | High; Locked by internal fabric plies |
| Conveyor Synchronization | Susceptible to micro-slip under high loads | High-Precision; Positive wedge engagement |
| Length Adjustability | Requires cutting and thermal welding | Manual interlocking; Zero tools required |
| Thermal Operating Envelope | Standard (-20°C to 180°F / 80°C) | Extended (Up to 194°F – 230°F / 90°C – 110°C) |
| Maintenance Protocol | Full loop extraction and replacement | Sectional replacement of individual links |
Operational Advantages and Trade-offs
Thermoplastic Polycords
-
Pros: Low initial component cost; exceptionally smooth operation at high rotational speeds; excellent absorption of minor mechanical shocks due to inherent material elasticity.
-
Cons: High tracking sensitivity; vulnerable to thermal aging near furnace entry/exit ports; time-intensive replacement procedures on long conveyor beds.
Interlocking Segment Belts
-
Pros: Eliminates conveyor shaft teardowns during installation; zero-slip transmission that protects fragile glass coatings; simplified logistics (one bulk spool accommodates any custom machine length).
-
Cons: Higher initial upfront investment per linear meter; requires a standard run-in period followed by a single link removal to compensate for initial mechanical bedding.
Decision Framework: Selecting the Optimal Drive Component
The choice between these two distinct drive systems should be dictated by the specific technical demands of the conveyor section:
-
Utilize circular section belts if you are outfitting ambient auxiliary transfer sections, cutting tables, or low-load pre-processing washing systems where operating temperatures remain stable and low component cost is the primary engineering driver.
-
Upgrade to tab-locked modular profiles if you are specifying components for the main drive roller beds of continuous glass tempering furnaces. The financial loss associated with a single batch of scratched low-E glass or an hour of unscheduled furnace downtime heavily outweighs the initial investment of a modular composite drive system.
Technical Specifications for Furnace Conveyor Upgrades
Managing thermal expansion and dust contamination on a glass production line requires specialized component engineering. Puteken provides both high-elasticity polyurethane round belts and high-durability adjustable link V-belts configured specifically for severe-service industrial environments.
Our furnace-optimized link series features an upgraded polymer compound designed to withstand continuous operating temperatures of 194°F to 230°F (90°C to 110°C) without glazing or structural deformation, ensuring consistent torque transfer to ceramic rollers.
For technical evaluations, dimensional cross-section layouts, or to explore component compatibility for automated glass lines, please coordinate with our technical support division through the Puteken Application Engineering Portal.